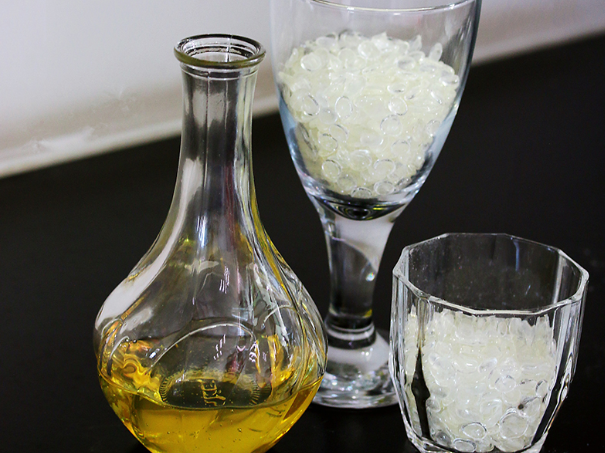
Comparative Insight: The One Variable That Breaks Production
The plant floor is unforgiving; a narrow change in melt viscosity turns a steady line into chaos. In that bleak light, comparative insight separates what holds from what cracks. I compare rosin-based tackifiers against synthetic tackifying resin blends because their viscosity-temperature curves behave differently under shear and thermal stress — and that matters for packaging runs and automotive assembly lines in Detroit where uptime is money. The first practical point is simple: set your viscosity band early and refuse excursions. tackifying resin performance is not a suggestion; it prescribes pump selection and nozzle geometry on the spot.
Processing Constraints in Hot-Melt Formulations
Hot-melt systems demand predictable melt index and thermal stability. Bulk rosin ester tackifier chemistry gives strong initial tack but often narrows the safe processing window: viscosity climbs fast as temperature drops, and shear-thinning behavior can hide problems until a shift change. Process engineers must monitor melt temperature, shear rate and residence time. Use a torque or inline viscometer to track real-time viscosity and trigger alarms before nozzle starvation occurs. Thermal degradation shows up as color shift and a falling molecular weight—both kill lap shear and long-term bond integrity.
Operational Production Teardown — What I Inspect
When I walk a line, I look at three tangible things: pump sizing relative to peak viscosity, heater control granularity, and filtration strategy. The teardown always includes an operational run sheet where we log viscosity at setpoints, nozzle backpressure, and cycle time. This is where I drop concrete labels — {main_keyword} and {variation_keyword} appear in the run sheet as parameters for recipe control — to ensure reproducibility. Filtration pore size and melt pump clearance make the difference between clean application and intermittent bead failure.
Comparing Rosin vs. Alternatives
Rosin esters bring excellent initial tack and good adhesion to polar substrates, but they can suffer from narrow thermal windows and oxidation. Synthetic tackifiers or hydrogenated hydrocarbon tackifiers widen the processing window, trade slight tack for lower melt viscosity at a given temperature, and ease pump wear. Choose based on substrate, required open time, and expected service temperature. A comparative checklist helps: melt index at 150°C, viscosity at operating shear, and thermal degradation onset measured by color or GPC shifts.
Common Mistakes and Small Course Corrections
Teams often chase higher line speeds by raising temperature without validating viscosity at the nozzle. That short-sighted fix reduces viscosity in the melt but accelerates thermal breakdown — bonds fail later in service. Another frequent error is ignoring filtration; particulate builds up and mimics a viscosity rise, triggering needless process adjustments. A modest intervention — tighter PID loops and inline viscosity trending — stabilizes runs with minimal capital spend.
Real-World Anchor and EEAT
From my audits on Midwest packaging lines to controlled lab trials, the pattern holds: predictable viscosity-temperature profiling prevents most failures. EEAT mode here is Practical Technical Guidance — backed by process logs from high-volume plants and material batch records. This is not theory; it echoes documented production downtimes where an untracked viscosity drift cost hours of rework on an automotive adhesive cell.
Advisory: Three Golden Rules for Selection and Control
1) Metric: Maintain operating viscosity within ±10% of the validated setpoint at the nozzle — measure at target shear rate rather than just temperature. 2) Metric: Specify melt index and thermal degradation onset for the tackifier batch; require these parameters in the certificate of analysis with explicit test conditions (e.g., melt flow rate at 150°C, 2.16 kg; thermal oxidation onset measured by TGA ramp at 10°C/min). 3) Metric: Implement inline filtration limits and pump clearances tied to particle size — state maximum acceptable particulate as <50 µm for critical nozzles and define replacement intervals in cycles per million units produced.
Closing Reflection
The comparative view leaves a clear route: control viscosity, choose the right tackifier chemistry, and harden your sensing. KOMO’s approach to materials and process control aligns with that route — practical, guarded, effective. KOMO
— a final note: precision keeps lines running; complacency does not.